1-805-484-2992
Quotes - Sizing - SalesOverview
A still's condenser has to knock vapor back to liquid fast enough to keep pace with the boiler, or the run backs up.
Distillation runs on removing heat as fast as the boiler adds it: the column or pot still's condenser has to knock vapor back to liquid at whatever rate the still is producing it, and a condenser that can't keep up either backs the run up or lets vapor escape uncondensed. Glycol gives a distillery a lower, steadier condensing temperature than a plain water loop, which tightens the cut between heads, hearts and tails.
Reflux and dephlegmator cooling on a column still adds a second, separate glycol duty on top of the final condenser - both draw off the same loop, but a column run often needs a colder setpoint on the reflux side than the final product condenser needs. Sizing has to account for both circuits, not just the total gallons produced per run.
Because a distillery's cooling demand often spikes hard during an active run and sits idle between batches, a right-sized portable or outdoor packaged glycol chiller - not an oversized central system - is usually the better fit for craft and mid-size operations.
- Condenser duty has to match the boiler's vapor rate, not lag behind it
- Reflux/dephlegmator cooling on column stills is a separate, often colder circuit
- Batch-cycle demand (hard peak, idle between runs) usually favors portable over central
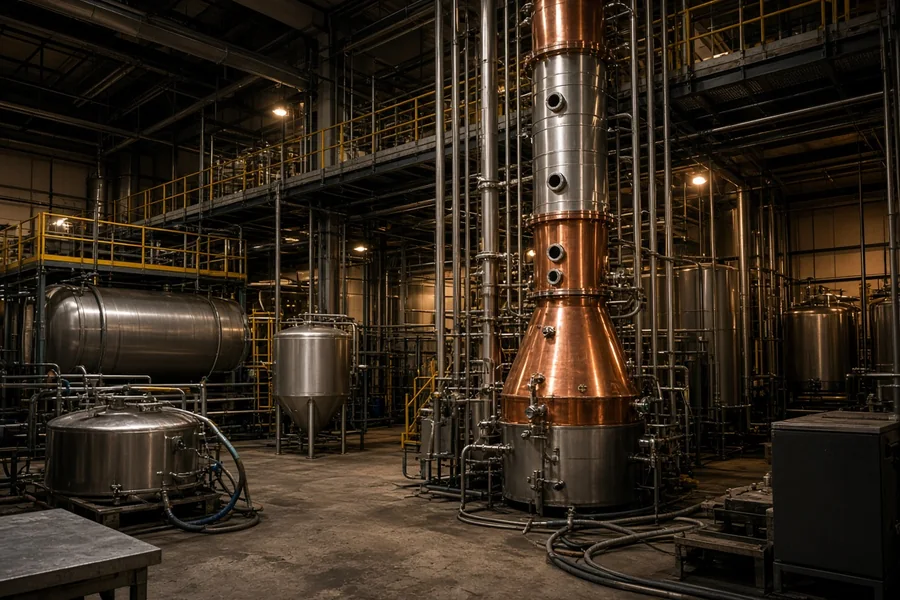
Sizing Distillery Condensing & Column Cooling
Condenser duty is a continuous load that tracks the still's boil rate directly - undersize it and the condenser can't knock vapor back to liquid fast enough, which backs up the run and can push uncondensed vapor past the condenser entirely. Column cooling, where a still uses one, adds a second, related demand for reflux control.
Because condensing load scales with boiler output rather than batch count, the number that matters most is your still's rated boil-off rate, not a generic per-batch estimate - send it to us along with your target condenser outlet temperature.
Send Us
- Still boil-off rate / boiler output
- Target condenser outlet temperature
- Column cooling requirement, if applicable
- Indoor or outdoor installation
TYPICAL RANGES BY DUTY
| Duty | Leaving Fluid Temp | Load Profile | Typical Glycol Mix |
|---|---|---|---|
| Primary condenser | 28-40°F | Continuous, boil-rate driven | 25-35% propylene |
| Reflux / column cooling | 35-45°F | Continuous, moderate | 20-25% propylene |
| Product cooling / proofing | 40-50°F | Batch | 15-20% propylene |
Ranges are typical starting points, not a substitute for a load calculation - actual leaving fluid temperature and glycol percentage depend on your still design, boil-off rate and spirit type.
Call and talk it through with an engineer: 1-805-484-2992.